X
we'll ensure you
always get best
results.
contact usGO

Hebei Weimiao Import and Export Trade Co., Ltd. specializes in R&D, marketing, pharma API manufacturing, and pharmaceutical intermediates, we have two affiliated bulk drug manufacturers. More than 70 percent of API pharma products are exported to Europe, America, Japan, and Southeast Asia.

Our factory is located in Hebei, a beautiful coastal city in the east region of China.

know more about company
Hebei Weimiao Biology Co., LTD
explore our news

Hebei Weimiao Import and Export Trade Co., Ltd. is a specialized and dynamic company dedicated to the research and development, manufacturing, and marketing of APIs (Active Pharmaceutical Ingredients) and pharmaceutical intermediates. With a commitment to excellence, we strive to deliver high-quality bulk pharmaceutical products that meet stringent industry standards. Our expertise lies in the production of essential components for the pharmaceutical sector, contributing to the advancement of healthcare solutions. Trust in Hebei Weimiao for reliable and innovative solutions in the field of API and pharmaceutical intermediate manufacturing.

  • Quality Control Evolution in Modern Biochemical Raw Materials

    Quality Control Evolution in Modern Biochemical Raw Materials

    Selecting a reliable carbomer 940 cas number Supplier requires a deep understanding of analytical quality control and compliance frameworks. The biochemical and fine chemical sectors are undergoing a significant transformation, shifting from basic material provision to highly integrated, technology-driven supply chains. For downstream formulators in the pharmaceutical and cosmetic industries, the consistency of raw materials directly dictates the stability, bioavailability, and regulatory success of the final product.

    0d4b66a06242b4bf5389e2e3aefcbdd5-20260310005433-转换自-webp.png

    The Imperative of Multi-System Certification

    In today's globalized market, raw materials must meet intersecting international standards. Products that fully comply with United States Pharmacopeia (USP), British Pharmacopoeia (BP), and European Pharmacopoeia (EP) guidelines provide a necessary foundation of trust. An advanced supplier does not merely trade chemicals; they operate robust in-house laboratories to conduct rigorous testing before exportation. This commitment to quality acts as a technical barrier, ensuring that only premium-grade intermediates reach global pharmaceutical industry leaders.

    Bridging the Gap: From Grams to Tonnage

    Scaling up the synthesis of active ingredients or plant extracts without compromising molecular integrity is a complex engineering challenge. Whether sourcing a highly specific reagent or evaluating a bulk Tocopherol supplier, buyers must scrutinize the manufacturer's capacity for seamless scalability. High-quality providers solve this by closely cooperating with GMP and FDA-qualified domestic facilities, coupled with research partnerships with prominent university laboratories.

    Strategic Logistics in Chemical Supply

    A sophisticated product requires an equally sophisticated delivery mechanism. Tailored multimodal logistics channels—including sea-air transport and dedicated cold chain routes—ensure that sensitive biochemicals maintain their purity from the factory to the client's facility. By prioritizing these comprehensive quality and logistical systems, modern enterprises provide long-term, high-value solutions to global markets.

    details
  • Harmonizing Biological and Targeted Chemical Strategies in Modern Agriculture

    Harmonizing Biological and Targeted Chemical Strategies in Modern Agriculture

    Advanced slayer thiamethoxam applications form a critical baseline for modern pest management, especially when integrating biological farming initiatives. As global agriculture shifts towards more sustainable and ecologically balanced practices, the intersection of biopesticides and highly targeted chemical crop protection has become a focal point for agronomists and bio-technologists alike. It is no longer about total eradication, but rather precision management.

    The Evolution of Integrated Pest Management (IPM)

    Historically, broad-spectrum applications often disrupted local microbiomes and beneficial insect populations. Today, the strategy has evolved. Agronomists now rely on a nuanced approach where biological controls—such as beneficial microbes and organic soil amendments—are supported by highly selective chemical interventions. This dual approach ensures that while the soil health remains vibrant, devastating pest outbreaks that biologicals cannot handle alone are swiftly neutralized. The chemical formulations utilized must boast exceptional purity and systemic efficiency to prevent residual environmental impact.

    Effective Vegetation Management Using Aquatic Weed Killer 2 4 D

    Synergy Through Advanced Technical Formulations

    The success of this balanced ecosystem heavily depends on the molecular stability of the applied treatments. When invasive species threaten crop viability, deploying specialized solutions like akarisida abamectin helps manage resistant mite populations without disrupting the entire biological ecosystem. Producing these sophisticated agro-industrial raw materials requires an advanced supplier with state-of-the-art synthesis capabilities.

    A premium manufacturer does not merely mix ingredients; they engineer solutions. Through meticulous quality control, precise crystallization, and optimized solubility parameters, these high-tier chemical components serve as the reliable backbone for hybrid agricultural programs. By securing materials from top-tier R&D-driven facilities, the agricultural sector can maintain crop yields while honoring the delicate balance of the farm's biological framework.


    details
we advice to choose
a right decision
  • our products
service_img
we'll ensure you always get
best results.
latest case studies

Hebei Weimiao Import and Export Trade Co., Ltd. showcases its strengths in precision manufacturing, customization, and global regulatory compliance, positioning itself as a reliable api pharmaceutical company and pharmaceutical intermediates manufacturer.

Inquiry for pricelist

Since its establishment, our factory has been developing first world class products with adhering the principle of quality first. Our products have gained excellent reputation in the industry and valuabletrusty among new and old customers..

submit now
latest blogs
view more
  • The Chemistry Behind Poultry Health: Raw Materials and Quality Standards in Veterinary Medicine

    2026-08-28

    The Chemistry Behind Poultry Health: Raw Materials and Quality Standards in Veterinary Medicine

    The Chemistry Behind Poultry Health: Raw Materials and Quality Standards in Veterinary Medicine

    Anti Diarrhea Powder is a fundamental formulation in poultry medicine, yet its effectiveness is intrinsically linked to the quality of active pharmaceutical ingredients and the manufacturing processes involved. The veterinary pharmaceutical industry relies on a complex supply chain of raw materials, chemical intermediates, and specialized production facilities to deliver safe and efficacious products.

    Veterinary pharmaceutical production line with quality control testing

    The global poultry industry has grown substantially over the past decade, with increasing demand for protein-rich food driving the need for effective veterinary interventions. This growth has placed greater scrutiny on the chemical compounds used in veterinary medicine, from basic feed additives to advanced therapeutic formulations. The quality of raw materials directly impacts not only the efficacy of these products but also food safety and public health.

    The Importance of Raw Material Quality in Veterinary Pharmaceuticals

    In veterinary medicine, the active pharmaceutical ingredients (APIs) and excipients used must meet stringent purity standards. Impurities or variations in chemical composition can lead to reduced efficacy, adverse reactions, or even toxicity in animals. This is particularly critical for formulations used in food-producing animals, where residues can enter the human food chain.

    Manufacturers that adhere to current Good Manufacturing Practice (cGMP) standards implement rigorous quality control measures at every stage of production. From raw material sourcing to final product testing, each step is documented and verified. Companies like Shimu Group, which has maintained GMP certification since 2005 and updated it in 2022, demonstrate the industry's commitment to quality assurance. Their 14 production lines, covering everything from powders and premixes to injections and infusions, reflect the complexity of modern veterinary pharmaceutical manufacturing.

    Chemical Standards and Regulatory Compliance in Veterinary Medicine

    The regulatory landscape for veterinary pharmaceuticals has become increasingly rigorous. International standards require manufacturers to demonstrate consistent product quality through validated processes and comprehensive testing. This includes raw material identification, potency assays, impurity profiling, and stability studies. For distributors and formulators working with chemical raw materials, understanding these regulatory requirements is essential for selecting reliable supply partners.

    Meloxicam Injection exemplifies the need for precise chemical formulation in veterinary medicine. As a non-steroidal anti-inflammatory drug used in both poultry and livestock, its efficacy depends on accurate dosing, proper formulation, and consistent manufacturing. The chemical stability of meloxicam in solution requires careful control of pH, excipients, and sterilization processes, highlighting the technical expertise required in veterinary pharmaceutical production.

    The Role of Research and Development in Veterinary Formulations

    Advancements in veterinary medicine are driven by research and development collaborations between industry and academia. Partnerships with agricultural universities and research institutions enable manufacturers to refine their formulations, develop new delivery systems, and improve the bioavailability of active compounds. These collaborations focus on optimizing chemical processes to enhance product stability, shelf life, and therapeutic outcomes.

    For the chemical raw materials industry, this means that demand for high-purity intermediates and specialized excipients continues to grow. Manufacturers that invest in R&D capabilities are better positioned to meet evolving market needs and regulatory requirements. The integration of advanced analytical techniques, such as HPLC and mass spectrometry, into quality control processes ensures that every batch meets predetermined specifications.

    Global Supply Chain Considerations for Veterinary Raw Materials

    The veterinary pharmaceutical industry operates on a global scale, with raw materials sourced from multiple regions. This international supply chain presents both opportunities and challenges. While it allows manufacturers to access specialized chemicals and competitive pricing, it also requires careful vendor qualification and supply chain management. Political instability, shipping disruptions, and changing regulatory requirements can all impact the availability of critical raw materials.

    Manufacturers that have established long-term relationships with reliable suppliers and maintain multiple sourcing options are better equipped to navigate these challenges. The trend toward vertical integration and strategic partnerships in the veterinary pharmaceutical industry reflects the importance of supply chain resilience. Companies with diversified production capabilities, such as those operating across multiple dosage forms and therapeutic categories, can offer greater stability to their partners.

    Future Trends in Veterinary Pharmaceutical Chemistry

    The future of veterinary medicine will likely see continued emphasis on formulation science, with a focus on improving bioavailability, reducing dosing frequency, and enhancing palatability. Nanotechnology, controlled-release formulations, and combination products are areas of active research. These innovations will require new chemical intermediates and specialized manufacturing capabilities, creating opportunities for raw material suppliers and contract manufacturers alike.

    Sustainability is also becoming a key consideration in veterinary pharmaceutical production. Green chemistry principles, waste reduction, and energy-efficient manufacturing processes are increasingly important to both regulators and end-users. Manufacturers that invest in sustainable practices while maintaining product quality will be well-positioned for long-term success in this evolving industry.

    In conclusion, the veterinary pharmaceutical industry's reliance on high-quality chemical raw materials and rigorous manufacturing standards underscores the importance of partnership between raw material suppliers and finished product manufacturers. As the global demand for safe, effective veterinary medicines continues to grow, the chemical industry's role in supporting animal health will remain indispensable.

    details
  • The Hidden Chemistry Behind Modern Skincare: How Peptide Raw Materials Are Reshaping Formulations

    2026-08-25

    The Hidden Chemistry Behind Modern Skincare: How Peptide Raw Materials Are Reshaping Formulations

    The Hidden Chemistry Behind Modern Skincare: How Peptide Raw Materials Are Reshaping Formulations

    Lipo-C 30MG represents a significant advancement in cosmetic ingredient delivery systems, offering enhanced stability and bioavailability for formulators on the cutting edge of skincare innovation. This lipid-encapsulated vitamin C derivative exemplifies how raw material chemistry continues to evolve to meet the demands of modern cosmetic science.

    Cosmetic peptide raw materials and chemical ingredients for skincare formulation

    Beauty and personal care have entered a new era where ingredient transparency and scientific backing are no longer optional—they are expected. Consumers are reading labels, questioning sourcing, and demanding formulations that deliver real, measurable results. This shift has placed raw material suppliers and cosmetic chemists under the spotlight, driving a wave of innovation in peptide chemistry, bio-fermentation, and green synthesis.

    The Rise of Bioactive Peptides in Cosmetic Formulations

    Peptides have moved from a niche ingredient category to a cornerstone of modern anti-aging and skin repair products. These short chains of amino acids act as signaling molecules, instructing skin cells to produce more collagen, reduce inflammation, or defend against environmental stressors. The global demand for cosmetic peptides has surged, with formulators seeking reliable, high-purity sources that can deliver consistent results across different product bases.

    What makes peptides particularly compelling is their versatility. From copper peptides that accelerate wound healing to matrixyl-inspired sequences that boost firmness, the range of functions is broad. However, the real challenge lies not in the concept but in the execution: manufacturing stable, bioavailable peptides at scale while maintaining cost efficiency and environmental responsibility.

    This is where the raw material supply chain becomes critical. Peptide synthesis requires precise control over reaction conditions, purification steps, and quality assurance protocols. Buyers in the beauty industry are increasingly auditing their suppliers for certifications, heavy metal testing, and batch-to-batch consistency. The days of accepting a certificate of analysis at face value are fading; instead, brands are demanding full transparency from factory to finished product.

    Why Raw Material Sourcing Matters More Than Ever

    The ingredient supply chain for cosmetics is global, complex, and increasingly scrutinized. A formulation is only as good as the raw materials that go into it. Impurities, inconsistent activity, or poor solubility can derail even the most thoughtfully designed product. This is especially true for peptide-based ingredients, where molecular integrity directly impacts efficacy.

    Consider the growing interest in BPC 157 10mg+GHK-CU 50mg+TB500 10mg combined peptide blends. These multi-peptide formulations are gaining traction among advanced skincare developers who want to address multiple skin concerns—repair, regeneration, and protection—in a single ingredient system. The complexity of combining different peptides while maintaining stability and synergy requires deep expertise in peptide chemistry and manufacturing.

    Brands that invest in understanding their raw material supply chain gain a competitive edge. They can trace each ingredient back to its origin, verify production methods, and ensure that sustainability claims are backed by data. This level of diligence builds trust with consumers and regulators alike, particularly as markets like the EU and the US tighten requirements for cosmetic ingredient safety and traceability.

    Green Synthesis: The New Standard in Peptide Manufacturing

    Environmental sustainability is no longer a marketing afterthought—it is a core requirement for raw material suppliers serving the beauty industry. Green synthesis methods, which minimize solvent use, reduce waste, and lower energy consumption, are becoming the benchmark for responsible peptide production. These approaches align with the broader cosmetics industry shift toward clean beauty, refillable packaging, and carbon-neutral operations.

    For peptide factories, adopting green chemistry principles means rethinking every stage of production: from protecting group strategies in solid-phase synthesis to solvent recovery systems and water recycling in purification. The result is a product that not only performs well but also meets the environmental standards that increasingly define brand identity. Suppliers that can demonstrate certified green manufacturing processes are positioned as preferred partners for forward-thinking beauty brands.

    This shift also creates opportunities for smaller, specialized factories to compete with larger commodity producers. By offering custom synthesis services, small-batch production runs, and collaborative R&D support, agile suppliers can help brands develop proprietary peptide sequences that differentiate their product lines. The ability to scale from lab-scale synthesis to commercial production while maintaining quality and sustainability is a valuable capability in the current market.

    Navigating Quality Control in Peptide Raw Materials

    Quality control in peptide manufacturing extends far beyond basic purity measurements. High-performance liquid chromatography (HPLC), mass spectrometry, and amino acid analysis are standard tools, but sophisticated buyers are also looking at endotoxin levels, microbial limits, and residual solvent profiles. For peptides intended for topical use, the stability of the molecule in different formulation matrices—creams, serums, gels—must be validated before commercial release.

    One often overlooked aspect is the importance of batch-to-batch consistency. A formulation that works perfectly with one batch of peptide raw material may fail with another if the activity profile shifts even slightly. This is why established suppliers invest in rigorous in-process controls and final-release testing that goes beyond regulatory minimums. For brands, partnering with a factory that can provide detailed stability data and technical support for formulation development is a significant advantage.

    The role of third-party testing and certification is also growing. Independent labs that verify supplier claims add an extra layer of trust, especially for brands entering new markets with different regulatory requirements. Suppliers that proactively share third-party audit reports and certification documents demonstrate a commitment to transparency that resonates with discerning buyers.

    The Future of Peptide Ingredient Innovation

    Looking ahead, the peptide raw material landscape will continue to evolve in response to consumer trends and scientific advances. Personalized skincare, microbiome-friendly formulations, and climate-adaptive products are all areas where peptides can play a central role. The ability to design peptides that target specific skin types, age groups, or environmental conditions will become a key differentiator for ingredient suppliers.

    Another frontier is the integration of peptide ingredients with advanced delivery systems—liposomes, nanoparticles, and bio-adhesive polymers—that improve penetration and prolong activity at the target site. These technologies require close collaboration between peptide chemists and formulation scientists, underscoring the value of suppliers that offer both raw materials and application expertise.

    For cosmetics brands, the message is clear: the quality and innovation of your products depend on the strength of your raw material partnerships. Building relationships with peptide factories that combine scientific depth, manufacturing excellence, and sustainability commitment is a strategic investment in long-term brand success.

    As the industry continues to raise the bar for ingredient performance and transparency, the role of specialized peptide manufacturers will only grow. Those who invest in green chemistry, rigorous quality systems, and collaborative innovation will define the next generation of skincare raw materials—and the products that rely on them.

    details
  • The Chemistry of Clean Beauty: How Raw Material Quality Defines Cosmetic Excellence

    2026-08-24

    The Chemistry of Clean Beauty: How Raw Material Quality Defines Cosmetic Excellence

    The Chemistry of Clean Beauty: How Raw Material Quality Defines Cosmetic Excellence

    Foot Spa Pedicure Jelly formulations rely on meticulously sourced raw materials that must satisfy rigorous safety and performance standards before reaching consumers. The global cosmetics industry has experienced a fundamental transformation, driven by increasingly informed consumers and stricter regulatory frameworks that demand complete transparency in ingredient sourcing and manufacturing protocols.

    Raw materials and ingredient quality control in cosmetics manufacturing laboratory

    The path from raw material to finished cosmetic product is complex and requires rigorous quality assurance at every stage. Manufacturers that invest in robust sourcing strategies and maintain strict quality control protocols are better positioned to deliver products that meet both safety expectations and performance requirements.

    The Foundation of Cosmetic Safety: Raw Material Selection

    Selecting high-quality raw materials is the single most critical factor in cosmetic product development. Every ingredient—whether emulsifier, surfactant, preservative, or active compound—must be evaluated for purity, stability, and compatibility with other formulation components. Impurities or inconsistencies in raw materials can compromise product safety, reduce efficacy, and lead to batch failures that carry significant financial and reputational consequences.

    Industry leaders prioritize suppliers who can provide detailed documentation of material provenance, chemical composition, and third-party testing results. This level of scrutiny is especially important for ingredients used in products intended for sensitive skin or children's care, where safety margins are understandably narrower.

    Certification Standards as Quality Benchmarks

    International certifications serve as essential reference points for evaluating raw material and manufacturing quality. Standards such as GMP (Good Manufacturing Practices), ISO 22716 (Cosmetics GMP), and FDA registration provide a framework for consistent quality management across the supply chain. Manufacturers that achieve these certifications demonstrate a commitment to operational excellence that extends from raw material receiving through final product dispatch.

    The presence of multiple certifications—including GMPC, ISO 22716, FDA, and SGS—indicates a manufacturer's comprehensive approach to quality assurance. These credentials are particularly valuable for companies serving international markets, where regulatory requirements vary significantly between regions. A certified facility with documented quality systems can more efficiently navigate the compliance landscape of different target markets.

    Innovations in Natural and Sustainable Ingredients

    The shift toward natural and sustainable ingredients has reshaped raw material sourcing strategies across the cosmetics industry. Plant-derived emollients, naturally occurring preservatives, and bio-based surfactants are increasingly replacing synthetic alternatives, driven by consumer demand for cleaner formulations. However, natural ingredients present unique challenges in terms of batch-to-batch consistency, stability, and preservation—requiring manufacturers to develop specialized expertise in their handling and formulation.

    100% Natural Body Butter formulations exemplify the growing demand for products that combine effective moisturization with clean ingredient profiles. The development of such products requires careful selection of plant-based butters and oils that deliver sensory appeal while maintaining stability without synthetic additives. This trend toward natural formulations has pushed manufacturers to deepen their understanding of raw material chemistry and invest in advanced processing capabilities.

    Supply Chain Resilience in Cosmetics Manufacturing

    The cosmetics industry's reliance on a global network of raw material suppliers makes supply chain management a strategic priority. Disruptions—whether from geopolitical events, shipping delays, or raw material shortages—can halt production lines and delay product launches. Manufacturers with diversified supplier networks and strategic inventory management practices are better equipped to maintain continuity in the face of such challenges.

    Established manufacturers with extensive industry experience bring valuable perspective to raw material sourcing and quality assurance. Hebei Enyu Imp. & Exp. Trade Co., Ltd, with over 13 years of specialization in cosmetics and personal care manufacturing, operates state-of-the-art facilities spanning 40,000 square meters and maintains GMPC, ISO 22716, and FDA certifications. The company's six dedicated production lines, including specialized workshops for bath bombs, bath salts, handmade soaps, and gift set assembly, demonstrate the infrastructure required to meet diverse market demands while maintaining rigorous quality standards.

    Quality Control Protocols and Brand Protection

    Effective quality control extends beyond raw material testing to encompass in-process monitoring, finished product evaluation, and stability testing. Manufacturers that implement comprehensive quality management systems can identify potential issues early, reducing waste and ensuring that only products meeting specifications reach the market. Brand protection measures, including secure supply chain documentation and traceability systems, further safeguard product integrity and consumer trust.

    The ability to produce over 10,000 sets of products daily while maintaining consistent quality requires sophisticated quality control infrastructure and trained personnel. Manufacturers who serve major retail chains like Wal-Mart, Tesco, Costco, and Disney have demonstrated their capacity to meet the stringent quality and compliance requirements of global retail partners.

    The Future of Cosmetics Raw Materials

    Looking ahead, the cosmetics industry will continue to evolve in response to technological innovation, regulatory changes, and shifting consumer preferences. Biotechnology-derived ingredients, advanced preservation systems, and sustainable packaging materials represent areas of active development. Manufacturers that invest in R&D capabilities and maintain flexible production infrastructure will be best positioned to capitalize on these emerging opportunities.

    The relationship between raw material quality and finished product excellence remains the cornerstone of the cosmetics industry. As the market continues to demand higher standards of safety, sustainability, and efficacy, the manufacturers who prioritize material science expertise and quality management will lead the way in shaping the future of personal care.

    details
  • The Critical Role of Industrial Minerals in Modern Chemical Manufacturing

    2026-08-21

    The Critical Role of Industrial Minerals in Modern Chemical Manufacturing

    The Critical Role of Industrial Minerals in Modern Chemical Manufacturing

    Kaolin Clay is a cornerstone material in the chemical industry, valued for its inertness, whiteness, and fine particle size. From ceramics and paints to pharmaceuticals and rubber, this layered silicate mineral provides essential functional properties that manufacturers depend on for consistent product quality.
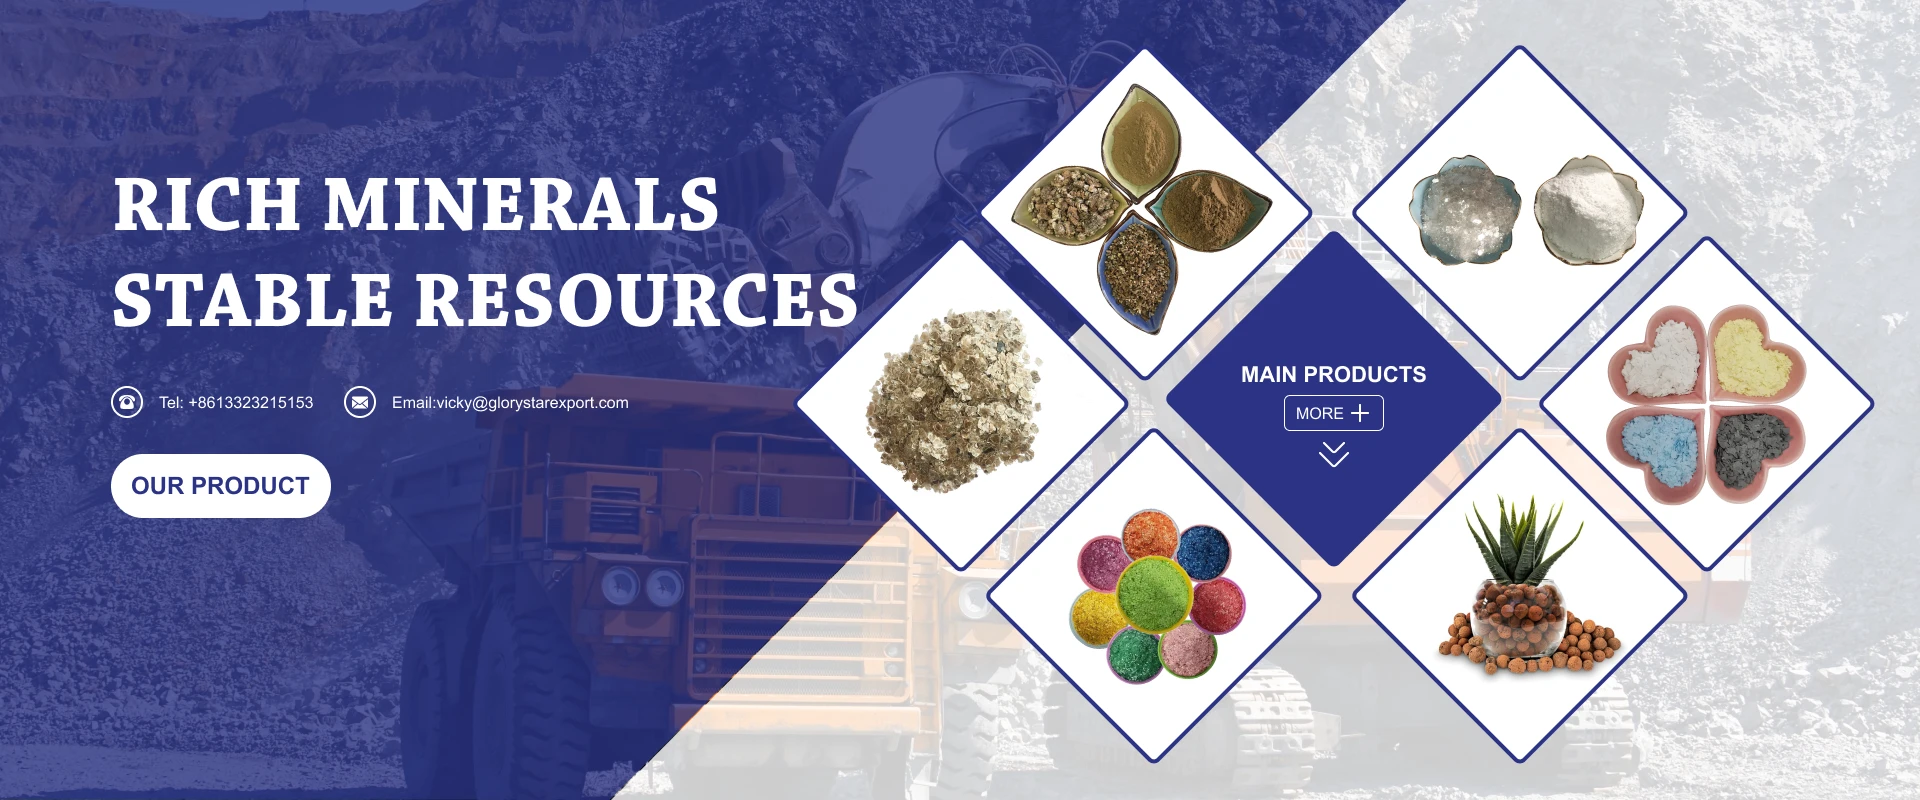
    Industrial mineral processing and quality control in chemical manufacturing

    Beyond kaolin, the broader family of non-metallic minerals — including bentonite, talc, diatomite, calcium carbonate, and barite — serves as the hidden backbone of countless chemical formulations. These raw materials influence everything from viscosity and opacity to thermal stability and abrasion resistance. As global chemical manufacturers push for higher performance and tighter regulatory compliance, the quality and consistency of these mineral inputs have never been more critical.

    Why Raw Material Quality Shapes Finished Product Performance

    In chemical manufacturing, the journey from raw material to finished product passes through multiple stages where variability can compound. A slight shift in mineral particle size distribution or trace element composition can alter reaction kinetics, change color profiles, or weaken structural integrity. This is why leading producers implement rigorous, multi-stage quality control systems that test incoming raw materials, in-process slurries, and final stored product before shipment.

    The most reliable mineral suppliers follow a four-point inspection protocol: first, testing raw materials upon arrival at the plant; second, conducting quality checks during active production; third, verifying specifications before warehouse storage; and fourth, performing a final spot check prior to loading. This layered approach, often aligned with ISO 9001:2015 management systems, minimizes the risk of off-spec material reaching the customer.

    Key Industrial Minerals and Their Chemical Applications

    Different minerals bring distinct value to chemical processes. Bentonite, with its high swelling capacity and ion-exchange properties, is widely used as a binder, thickener, and suspending agent in drilling fluids, foundry sands, and cosmetic formulations. Talc powder contributes lubricity, thermal stability, and reinforcement in plastics, paper, and coatings. Diatomite, a naturally porous silica, serves as a filtration aid, absorbent, and mild abrasive. Calcium carbonate, one of the most abundant minerals on earth, functions as a filler, extender, and pH buffer in paints, adhesives, sealants, and pharmaceuticals.

    Graphite Powder is another versatile material with growing importance in the chemical sector. Its high thermal conductivity, chemical inertness, and natural lubricity make it indispensable in high-temperature gaskets, conductive coatings, battery electrodes, and specialty lubricants. As the energy transition accelerates demand for advanced battery materials, the role of high-purity graphite continues to expand.

    Supply Chain Reliability in a Global Market

    Chemical manufacturers today face mounting pressure to secure stable, long-term supplies of high-quality mineral raw materials. Geopolitical disruptions, logistics bottlenecks, and variable ore grades from one region to another all introduce risk. Experienced buyers look for suppliers with deep reserves, established production history, and a track record of consistent export to demanding markets such as Japan, South Korea, the United States, Germany, and Australia.

    One noteworthy example is the Lingshou County region in China, a historic source of non-metallic minerals including mica, kaolin, and graphite. Factories with decades of operational experience, backed by dedicated R&D teams and national high-tech certifications, offer the kind of technical stability that global chemical buyers require. The presence of multiple national patents and active membership in local mineral associations further signals a commitment to continuous improvement and industry standards.

    Selecting the Right Mineral Partner for Long-Term Success

    When evaluating mineral suppliers, chemical manufacturers should prioritize three factors: demonstrated quality systems, production capacity, and technical expertise. ISO 9001 certification provides a baseline for process control, but the most reliable partners go further by investing in in-house testing laboratories and developing customized product grades for specific applications. A supplier with annual output exceeding 100,000 metric tons and a 35-year-plus operating history brings both scale and institutional knowledge that smaller operations cannot match.

    As the chemical industry continues to evolve — toward greener formulations, higher purity standards, and more complex performance requirements — the importance of high-quality mineral raw materials will only grow. By choosing partners who invest in technology, quality control, and long-term relationships, manufacturers can build supply chains that are both resilient and capable of supporting the next generation of chemical products.

    Editor’s Note: This article is part of an ongoing series examining the raw materials that underpin global chemical manufacturing. For further reading on mineral specifications and sourcing strategies, consult industry publications such as the Industrial Minerals Association and the American Chemical Society.
    details
  • Raw Material Sourcing in Specialty Chemical Manufacturing: Quality and Supply Chain Dynamics

    2026-08-21

    Raw Material Sourcing in Specialty Chemical Manufacturing: Quality and Supply Chain Dynamics

    Raw Material Sourcing in Specialty Chemical Manufacturing: Quality and Supply Chain Dynamics

    A Metal Candle Holder is a product that demonstrates the importance of raw material selection in specialty chemical manufacturing. The chemical industry relies on consistent, high-quality inputs to produce reliable finished goods across countless downstream applications.

    Specialty chemical raw material processing and quality control in industrial manufacturing

    The Critical Role of Raw Material Consistency

    In specialty chemical manufacturing, raw material consistency directly influences product performance, safety, and longevity. Whether formulating industrial adhesives, coatings, or composite materials, manufacturers depend on suppliers who can deliver uniform chemical properties batch after batch. Variability in raw material quality can lead to production downtime, increased waste, and compromised end-product reliability.

    The supply chain for specialty chemicals has grown increasingly complex. Global sourcing, fluctuating commodity prices, and evolving regulatory standards require manufacturers to maintain rigorous quality control protocols. Many leading producers now invest in advanced analytical testing — including spectrometry, chromatography, and thermal analysis — to verify raw material specifications before production begins.

    Emerging Trends in Material Selection and Certification

    Sustainability and traceability have become central to raw material procurement strategies. Chemical manufacturers are increasingly seeking certified raw materials that meet environmental and social responsibility standards. This shift is driven by both regulatory pressure and end-user demand for greener products. Recycled content, bio-based feedstocks, and low-carbon processing methods are gaining traction across the industry.

    At the same time, supply chain resilience has emerged as a top priority. The disruptions of recent years prompted many manufacturers to diversify their supplier base, increase safety stock levels, and invest in regional sourcing capabilities. These measures help mitigate risks associated with geopolitical instability, logistics bottlenecks, and raw material shortages.

    Material Quality Across Manufacturing Applications

    The specifications for raw materials vary significantly depending on the end application. In sectors such as automotive, aerospace, and consumer goods, material purity, mechanical strength, and thermal stability are non-negotiable. Even minor deviations in raw material composition can affect the performance of the final product, leading to costly recalls or safety issues.

    For example, metal and glass components used in decorative and functional products require precise material properties. A Glass Candle Holder must be manufactured from glass that can withstand thermal stress and maintain optical clarity. Similarly, metal components demand consistent alloy composition and surface finish to ensure durability and aesthetic appeal.

    Quality Control Frameworks in Raw Material Supply

    Established quality management systems such as ISO 9001 and IATF 16949 provide frameworks for raw material verification and supplier auditing. These standards require manufacturers to document material specifications, conduct incoming inspections, and maintain traceability records. Many chemical producers also implement statistical process control (SPC) to monitor material variability and identify trends that could impact product quality.

    Supplier partnerships have become more collaborative, with manufacturers and raw material providers working together to optimize material formulations. This cooperation often leads to innovation in material performance, cost reduction, and improved sustainability profiles. Long-term contracts and shared quality data further strengthen these relationships.

    The Path Forward for Specialty Chemical Sourcing

    As the specialty chemical industry continues to evolve, raw material sourcing will remain a cornerstone of manufacturing excellence. Companies that prioritize material quality, supply chain transparency, and sustainable practices will be better positioned to meet the demands of an increasingly discerning market. The integration of digital tools — from blockchain for traceability to AI for supplier risk assessment — will further enhance the reliability and efficiency of raw material procurement.

    Ultimately, the quality of the finished product is a direct reflection of the raw materials used. Whether in industrial chemicals, consumer goods, or decorative accessories, the commitment to material excellence drives long-term success across the entire value chain.

    details
  • High-Performance Chemical Additives Reshaping Construction and Industrial Applications

    2026-08-21

    High-Performance Chemical Additives Reshaping Construction and Industrial Applications

    High-Performance Chemical Additives Reshaping Construction and Industrial Applications

    A reliable water reducer plays a foundational role in achieving high-performance concrete for modern infrastructure, enabling stronger, more durable structures while reducing water content. As construction and industrial material formulations become increasingly sophisticated, chemical additives have evolved from simple functional ingredients into complex performance enablers that address rheology, workability, durability, and environmental impact. This transformation reflects broader shifts in how engineers, formulators, and specifiers approach material design across the built environment and beyond.

    Chemical additives and polymer powders for construction and industrial formulations

    The Expanding Role of Chemical Additives in Construction Materials

    Over the past decade, the construction chemicals market has experienced steady growth, driven by the need for higher performance standards, stricter environmental regulations, and the push for longer service life in buildings and infrastructure. Additives such as plasticizers, superplasticizers, retarders, accelerators, and viscosity modifiers are now standard components in concrete, mortar, grout, and cement-based systems. Among these, water-reducing agents have become particularly critical because they allow formulators to reduce the water-to-cement ratio without sacrificing workability, resulting in denser, stronger, and more durable concrete.

    The science behind these additives continues to advance. Modern polycarboxylate-based water reducers, for example, operate through a combination of electrostatic repulsion and steric hindrance, dispersing cement particles more effectively than traditional naphthalene or melamine-based alternatives. This enables lower dosages, better slump retention, and improved compatibility with a wide range of cement chemistries. For engineers working on high-rise buildings, bridges, tunnels, and precast elements, these performance gains translate directly into project efficiency and structural reliability.

    Beyond concrete, chemical additives are equally vital in dry-mix mortars, tile adhesives, self-leveling compounds, and repair systems. The ability to fine-tune open time, setting behavior, adhesion, and sag resistance depends on carefully selected additive packages that are tailored to specific application requirements and climatic conditions. This has led to a growing demand for customized solutions that address the unique challenges faced by local construction markets around the world.

    Key Applications Across Building Materials and Industrial Formulations

    The use of chemical additives extends well beyond concrete. In the production of gypsum-based products, plasters, and joint compounds, additives such as cellulose ethers and starch ethers are employed to control water retention, improve workability, and enhance adhesion. These materials are essential for achieving consistent application properties and final finish quality, particularly in mechanized spraying systems and large-scale construction projects.

    In the coatings and paints industry, chemical additives play a key role in pigment dispersion, rheology modification, and film formation. The same principles that govern concrete admixture performance also apply to the formulation of water-based paints, where stabilizers, thickeners, and dispersants are used to achieve the desired viscosity, leveling, and storage stability. The growing preference for low-VOC and environmentally friendly products has further accelerated the adoption of advanced additive technologies that meet both performance and sustainability goals.

    The detergents and personal care sector also relies heavily on specialty chemical additives. Thickeners, surfactants, and conditioning agents are formulated to deliver specific sensory experiences, cleaning efficacy, and product stability. Cellulose ethers, in particular, are valued for their ability to provide consistent viscosity across a broad pH range, making them indispensable in liquid soaps, shampoos, and household cleaning products. The cross-industry applicability of these materials underscores the importance of having a deep understanding of polymer chemistry and formulation science.

    Redispersible Polymer Powders and Their Impact on Modern Formulations

    Among the most versatile and widely used additives in dry-mix mortars and cementitious systems is Redispersible Polymer Powder (RDP). This free-flowing powder is produced by spray-drying polymer emulsions, and when re-dispersed in water, it forms a film that significantly improves the adhesion, flexibility, cohesion, and water resistance of the final material. RDP is a critical component in tile adhesives, exterior insulation and finish systems (EIFS), self-leveling underlayments, and repair mortars, where mechanical performance and long-term durability are paramount.

    The selection of the appropriate RDP grade depends on factors such as the desired glass transition temperature (Tg), film-forming ability, and compatibility with other components in the formulation. Advances in polymer chemistry have led to the development of RDPs with tailored properties, such as enhanced hydrophobic characteristics, improved alkali resistance, and better redispersion behavior. These innovations allow formulators to achieve performance levels that were previously unattainable with standard cementitious systems, opening up new possibilities for thin-bed applications, flexible waterproofing membranes, and decorative renders.

    The growing demand for energy-efficient buildings and sustainable construction practices has further highlighted the importance of RDPs. By improving the mechanical properties and durability of cement-based materials, these polymer powders contribute to longer service life, reduced maintenance costs, and lower embodied carbon over the building lifecycle. As regulations around building energy performance continue to tighten, the role of advanced polymer additives in achieving these targets will only become more pronounced.

    Quality Standards, Customization, and Supply Chain Reliability

    As the range and complexity of chemical additives continue to expand, the importance of consistent quality and reliable supply has never been greater. Formulators and construction material producers depend on raw material suppliers who can deliver products that meet stringent specifications batch after batch. This is particularly true for additives like cellulose ethers, redispersible polymer powders, and water-reducing agents, where minor variations in molecular weight, degree of substitution, or particle size can have a significant impact on end-use performance.

    Leading manufacturers in the specialty chemicals space have responded by investing in dedicated research and development centers, state-of-the-art production facilities, and rigorous quality control systems. Companies such as Shijiazhuang Yaguan New Material Technology Co., Ltd. have established themselves as trusted partners in the global supply chain by combining technical expertise with a commitment to innovation and customization. With a substantial production capacity and a focus on understanding customer needs, Yaguan offers one-stop sourcing services and product solutions that help formulators bring high-performance materials to market more efficiently.

    The ability to provide customized production and tailored technical support has become a key differentiator in the industry. Whether it is modifying the viscosity profile of a cellulose ether for a specific tile adhesive application or developing a unique polymer blend for a waterproofing membrane, the most successful suppliers are those that work closely with their customers to solve complex formulation challenges. This collaborative approach not only speeds up product development cycles but also fosters long-term partnerships that drive innovation across the entire value chain.

    For buyers and specifiers, selecting the right additive supplier is a strategic decision that goes beyond price and availability. Factors such as technical support, product consistency, regulatory compliance, and supply chain transparency are equally important. As the global construction and industrial materials market continues to evolve, the demand for high-quality, reliable, and customized chemical additives will remain a cornerstone of progress in the industry.

    The Future of Specialty Chemicals in Construction and Industry

    Looking ahead, several trends are shaping the future of chemical additives in construction and industrial applications. The push toward sustainability is driving the development of bio-based and biodegradable polymers, low-carbon cement alternatives, and additives that enable the use of recycled materials without compromising performance. Digitalization and data-driven formulation are also gaining traction, with machine learning and high-throughput screening accelerating the discovery of new additive combinations and optimized recipes.

    At the same time, the globalization of construction markets means that suppliers must be able to serve diverse climatic conditions, regulatory environments, and application standards. The ability to provide consistent quality across multiple regions, supported by local technical expertise and responsive logistics, will be a defining characteristic of leading chemical companies in the coming years. Collaboration between raw material producers, formulators, and end-users will be essential for addressing the complex challenges of modern construction and industrial manufacturing.

    In conclusion, the role of high-performance chemical additives in shaping the built environment and industrial products is both profound and growing. From water reducers that enable high-strength concrete to redispersible polymer powders that enhance the durability of thin-bed mortars, these materials are at the heart of innovation in the sector. As the industry continues to evolve, the partnerships between formulators and raw material suppliers will remain a vital force driving progress, quality, and sustainability.

    details
  • The Evolution of Textile Dyeing: Balancing Color Intensity with Sustainable Chemistry

    2026-08-17

    The Evolution of Textile Dyeing: Balancing Color Intensity with Sustainable Chemistry

    The Evolution of Textile Dyeing: Balancing Color Intensity with Sustainable Chemistry

    Indigo Blue Vat Blue chemistry remains the cornerstone of the global denim industry, driving much of the aesthetic demand in modern fashion. As consumer preferences shift toward high-quality, durable fabrics, the chemical complexity required to achieve deep, consistent shades has increased significantly.

    The textile manufacturing landscape is currently navigating a dual challenge: the necessity for vibrant, long-lasting coloration and the urgent regulatory pressure to reduce environmental footprints. For chemical engineers and textile manufacturers, this means moving beyond traditional application methods toward more precise, high-purity pigment and dye formulations.

    Industrial textile dyeing process and chemical pigment application

    Technical Challenges in Modern Coloration

    Achieving color fastness—the ability of a material to retain its color without fading or running—requires a sophisticated understanding of molecular bonding between the dye and the substrate. In denim production, where mechanical abrasion is a constant factor, the stability of the indigo molecule is critical.

    One of the primary technical hurdles is the management of oxidation during the dyeing process. When working with specialized derivatives like Bromo Indigo, manufacturers must maintain strict control over pH levels and redox potentials to ensure that the pigment integrates perfectly into the fiber structure. Any deviation can lead to uneven shading or reduced durability.

    The Shift Toward High-Purity Raw Materials

    The quality of the final textile product is directly proportional to the purity of the raw chemical inputs. Impurities in pigments or dyes can cause unexpected chemical reactions, affecting not only the color but also the structural integrity of the fabric. This has led to a greater reliance on specialized industrial partners who focus on high-precision manufacturing.

    "The global supply chain for specialty chemicals is moving toward a model of vertical integration, where the consistency of the raw pigment determines the efficiency of the entire textile mill."

    Sustainability and the Future of Pigments

    As environmental regulations like REACH and various local wastewater standards become more stringent, the industry is looking toward more efficient pigment technologies. The goal is to minimize "exhaustion loss"—the amount of dye that remains in the water rather than attaching to the fabric.

    Innovations in pigment green and pigment blue formulations are helping factories reduce their chemical oxygen demand (COD) in wastewater. By utilizing more concentrated, high-quality pigments, manufacturers can achieve the desired shade with less volume, thereby reducing the total chemical load on local water systems.

    Conclusion: The Role of Material Science

    The intersection of fashion and chemistry is more complex than ever. As the industry moves forward, the success of textile producers will depend heavily on the reliability of their chemical supply chains and the technical sophistication of the dyes and pigments they employ. Continuous research and development in molecular stability and environmental compatibility remain the most vital drivers of growth in this sector.

    details
  • Innovations and Challenges in Decorative Aggregates for Modern Construction

    2026-08-14

    Innovations and Challenges in Decorative Aggregates for Modern Construction

    Innovations and Challenges in Decorative Aggregates for Modern Construction

    decorative pea gravel continues to gain popularity as a versatile material in landscaping and flooring solutions due to its aesthetic appeal and functional benefits. As urban development and architectural trends evolve, the demand for innovative mineral-based aggregates that combine durability with design flexibility grows rapidly.

    Colorful decorative aggregates for flooring and landscaping

    Addressing Industry Pain Points: Quality, Sustainability, and Supply Chain

    The construction and chemical raw materials industry faces significant challenges including ensuring consistent quality, meeting environmental regulations, and maintaining a resilient supply chain. High-quality mineral aggregates such as natural color sand, glass sand, and quartz sand are essential components that influence the performance and longevity of finished products like terrazzo flooring and epoxy coatings. The sourcing and processing of these materials require advanced beneficiation and quality control techniques to meet stringent standards.

    Sustainability has become a pivotal concern as customers and regulators demand eco-friendly materials that reduce environmental impact. Innovations in mining and processing technologies now allow for more efficient extraction and refinement of mineral products, minimizing waste and energy consumption while preserving natural resources.

    Emerging Trends in Decorative Aggregates and Flooring Materials

    The aesthetic and functional versatility of aggregates has led to the rise of specialty products such as luminous stones for terrazzo, which add a unique glow-in-the-dark element to floors and surfaces. These innovative materials enhance design possibilities for architects and interior designers, combining safety features with visual appeal.

    Additionally, the integration of epoxy flakes and natural pebbles in flooring systems has expanded the market for durable, decorative finishes that withstand heavy foot traffic and environmental stressors. These materials often require precise particle size distribution and chemical purity, underscoring the importance of advanced mineral processing and laboratory testing.

    Supply Chain Dynamics and Quality Control in Mineral Products

    Reliable supply chains are critical to meet the diverse demands of global markets, especially when exporting to regions with different regulatory frameworks and quality expectations. The ability to offer tailored products such as natural color sand or white cobblestones requires a multi-layered management approach that includes beneficiation, packing, storage, and transportation logistics.

    Rigorous quality control protocols, supported by modern laboratory equipment and expert chemical analysis, ensure that products consistently meet customer specifications. This commitment to quality safeguards the integrity of flooring aggregates used in demanding applications, from residential landscaping to commercial terrazzo installations.

    Conclusion: The Future of Mineral-Based Decorative Materials

    As the construction and chemical raw materials sectors continue to innovate, the role of high-quality mineral aggregates becomes increasingly significant. The combination of aesthetic appeal, sustainability, and performance drives demand for products like decorative pea gravel and luminous stones for terrazzo. Industry players who invest in advanced processing technologies and maintain robust supply chains will be well-positioned to meet evolving market needs and regulatory requirements.

    Ultimately, collaboration between mining enterprises and downstream manufacturers fosters the development of superior materials that enhance both the beauty and functionality of modern construction projects worldwide.

    details
  • Innovations and Challenges in Chemical Additives for Construction Materials

    2026-08-13

    Innovations and Challenges in Chemical Additives for Construction Materials

    Innovations and Challenges in Chemical Additives for Construction Materials

    hpmc grades viscosity plays a crucial role in determining the performance of cellulose ethers in modern construction applications. These additives have become indispensable in improving workability, water retention, and durability of cementitious materials, especially in drywall, plaster, and tile adhesives.

    Industrial chemical production facility with advanced equipment

    Understanding the Role of Cellulose Ethers in Construction

    Cellulose ethers, including hydroxypropyl methylcellulose (HPMC), hydroxyethyl cellulose (HEC), and hydroxyethyl methylcellulose (HEMC), have gained prominence due to their ability to enhance the rheological properties of cement-based materials. The unique hpmc structure allows it to form a protective film around cement particles, which stabilizes the mixture and prevents segregation during application.

    These additives also significantly improve water retention, which is critical for proper hydration of cement and curing. This not only leads to stronger finished products but also reduces cracking and shrinkage, addressing common pain points in construction projects.

    Current Trends and Industry Challenges

    The construction chemical sector is evolving rapidly, with increasing demand for eco-friendly and high-performance materials. Manufacturers face the challenge of balancing cost-efficiency with product stability and environmental compliance. Additionally, the need for additives that perform well under diverse climatic conditions has intensified research into customized cellulose ether formulations.

    Another trend is the integration of advanced production technologies to ensure consistent quality and scalability. Automated control systems and stringent quality assurance protocols have become industry standards to meet the growing expectations of global markets.

    Ensuring Quality and Supply Chain Support

    Maintaining high-quality standards in cellulose ether production requires a comprehensive approach, including raw material selection, process control, and laboratory testing. For instance, the use of refined cotton as a cellulose source demands rigorous inspection and handling to preserve purity and performance characteristics.

    Advanced facilities equipped with reaction kettles, gas recycling systems, and dust collectors contribute to both environmental sustainability and product consistency. Water treatment and centralized control rooms further enhance operational efficiency and compliance with environmental regulations.

    Collaboration between chemical producers and construction material manufacturers is essential for tailoring solutions that meet specific project requirements. This partnership helps to optimize formulations and application techniques, ultimately improving the competitiveness of construction products in the market.

    Conclusion

    The construction industry continues to rely heavily on chemical additives like HPMC and related cellulose ethers to enhance material properties and project outcomes. Innovations in production technology and quality control are vital to address evolving market demands and regulatory challenges. By understanding the intricate relationship between additive structure and performance, stakeholders can drive forward more durable, sustainable, and efficient construction solutions.

    details
  • Bio-Stabilization and Texture Engineering in Modern Food Science

    2026-08-06

    Bio-Stabilization and Texture Engineering in Modern Food Science

    Bio-Stabilization and Texture Engineering in Modern Food Science

    Innovations in hpmc food grade hydrocolloids have transformed the formulation of plant-based alternatives and emulsified systems. Achieving structural parity with traditional animal proteins requires a nuanced understanding of polysaccharide interactions and thermal gelation properties.

    Mimicking Gluten Matrices and Emulsion Stability

    In gluten-free bakery and bio-engineered food matrixes, cellulose derivatives mimic the viscoelastic network normally provided by gluten. During heat processing, the reversible thermal gelation traps moisture and structural gases, preventing collapse and delivering optimal crumb texture and mouthfeel.

    Chemical Transparency and Standardized Identification

    Formulators evaluating raw ingredients often reference standardized registry identifiers, verifying parameters under specific chemical listings such as hpmc cas specifications. Regulatory transparency ensures that raw material purity complies with international food safety codes and biological compliance standards.

    2-2.png

    Sourcing High-Purity Bio-Compatible Additives

    As consumer demand for sustainable, plant-derived products grows, food technologists depend on an advanced supplier with specialized technical capabilities to deliver non-ionic cellulose derivatives that remain stable across broad pH and temperature ranges.

    details
  • Formulation Stability in Bio-Enzymatic Cleaning: Engineering the Perfect Chemical Matrix

    2026-08-03

    Formulation Stability in Bio-Enzymatic Cleaning: Engineering the Perfect Chemical Matrix

    Formulation Stability in Bio-Enzymatic Cleaning: Engineering the Perfect Chemical Matrix

    63227_0c0c2622-732f-411f-b3c2-4f8598677852-20251219032627-20260618223909.png

    Choosing a pure Detergent raw material is the foundational step in bio-formulation. Bridging the gap between biological efficacy and chemical stability is the holy grail of modern formulation science. The transition toward biotechnology in the industrial and consumer cleaning sectors is no longer an emerging trend; it is the established standard. Bio-enzymatic agents—specifically proteases, lipases, amylases, and cellulases—offer unparalleled catalytic efficiency. They can target and dismantle complex organic macromolecules at the molecular level, operating effectively at low temperatures and neutral pH levels. However, deploying these fragile biological proteins within harsh, commercially viable liquid environments presents monumental engineering challenges.

    The Fragility of Biological Catalysts

    To fully grasp the formulation challenge, one must first understand enzyme architecture. Enzymes are intricate, three-dimensional folded proteins composed of long chains of amino acids. Their remarkable cleaning power derives from a specific, highly specialized "active site" that acts as a lock-and-key mechanism for specific soils—for example, a protease binding specifically to the peptide bonds in a blood stain.

    If the delicate three-dimensional structure of the enzyme unfolds or alters—a process known as denaturation—the active site is irreversibly destroyed, and the enzyme becomes entirely inert. In a typical liquid cleaning formulation, enzymes are constantly under siege. Aggressive anionic surfactants, high alkalinity, and the presence of oxidative agents can disrupt the hydrogen bonds maintaining the enzyme's structure. Therefore, formulators must construct a highly protective chemical matrix that suppresses these antagonistic interactions while preserving the overall detergency and shelf-life of the product.

    The Mechanics of Surfactant-Enzyme Interaction

    The primary conflict in bio-cleaning formulas lies between the biological catalysts and the primary chemical surfactants. While enzymes break down specific soils chemically, surfactants are required to reduce surface tension, emulsify the broken-down soils, and keep them suspended in the wash water to prevent redeposition.

    However, many traditional, aggressive surfactants can penetrate the protein structure of the enzyme, causing rapid denaturation. To mitigate this, advanced formulations require carefully selected co-surfactants that provide high detergency without exhibiting protein-denaturing properties. The goal is to create a micellar structure in the liquid that encapsulates the enzymes, shielding them from reactive elements like free water molecules and trace heavy metals, until the product is diluted during the actual washing process.

    Rheology, Viscosity, and Foam Stabilization

    Beyond chemical compatibility, the physical properties of the liquid matrix—its rheology and viscosity—play a massive role in both enzyme suspension and consumer experience. A high-performance bio-cleaner must maintain a stable viscosity across a wide temperature range and produce a rich, stable foam profile when agitated. This is particularly crucial in applications like industrial surface cleaning or premium dishwashing liquids, where foam acts as a physical medium to hold the enzymes against the soiled surface for an extended dwell time.

    Achieving this precise physical state requires elite viscosity modifiers and foam stabilizers. The integration of 85% CDEA (Coconut Diethanolamide) is highly favored by top-tier formulators for this exact purpose. As a premium non-ionic surfactant, it excels at thickening liquid formulations without requiring high concentrations of inorganic salts (which can destabilize enzymes). Furthermore, it provides exceptional foam boosting and stabilization, creating a dense, luxurious lather that remains stable even in the presence of heavy greasy soils.

    Because it is non-ionic and incredibly stable, it integrates seamlessly into the protective micellar matrix, enhancing the physical properties of the cleaner without chemically antagonizing the delicate protease and lipase enzymes suspended within it.

    Conclusion: The Convergence of Biology and Materials Science

    The successful commercialization of high-performance bio-enzymatic cleaning products is an exercise in rigorous chemical balancing. It is not enough to simply add biotechnology to a traditional soap formula; the entire formulation must be re-engineered from the ground up. By utilizing advanced, highly compatible raw materials to control rheology, stabilize foam, and protect protein structures, developers can create resilient matrices that maximize biological efficacy. As the cleaning industry continues its pivot towards sustainable, high-efficiency solutions, mastery of this complex intersection between biology and surface chemistry will dictate the market leaders of the next decade.


    details
  • Optimizing Bioreactor Environments: The Impact of Precise pH Regulation in Biotechnology

    2026-07-30

    Optimizing Bioreactor Environments: The Impact of Precise pH Regulation in Biotechnology

    Optimizing Bioreactor Environments: The Impact of Precise pH Regulation in Biotechnology

    Controlling Cellular Metabolism

    Utilizing anhydrous acetic acid is fundamental for stabilizing bioreactor pH levels during complex biotechnological processes. In microbial fermentation and mammalian cell culture, the metabolic pathways are highly sensitive to even the slightest fluctuations in their chemical environment. As cells metabolize nutrients, they produce lactic acid and other metabolic by-products that naturally depress the pH of the culture medium. To prevent cell death and maintain high yields of target proteins or enzymes, bio-engineers must continuously introduce highly pure buffering agents to neutralize these shifts and sustain an optimal growth environment.

    Downstream Processing and Protein Purification

    Once the fermentation phase is complete, the focus shifts to downstream processing, where target molecules are separated and purified. Chromatography techniques often require precise buffer gradients to elute proteins without altering their delicate three-dimensional structures. The introduction of water or unknown impurities at this stage can be disastrous, leading to protein denaturation. Thus, utilizing an organic acid with ≥ 99.8% purity is essential to ensure that the chemical composition of the elution buffers remains absolutely consistent, safeguarding the integrity of the biologic product.

    Understanding Glacial Acetic Acid Appearance and Industrial Use

    Strategic Sourcing in Biochemical Engineering

    The success of commercial-scale biotechnology relies heavily on the quality of raw chemical inputs. The integration of high-grade glacial ethanoic acid provides a reliable, contaminant-free medium for biological regulation. To achieve reproducible results, biotech facilities must procure these critical reagents from an advanced supplier capable of guaranteeing chemical stability and exact technical specifications, such as a refractive index of 1.3716. High-quality providers ensure that the foundational chemicals introduced into the bioprocess meet both structural and regulatory demands, ultimately driving innovation in modern bio-manufacturing.

    details
  • Enhancing Downstream Bioprocessing with Specialty Chemistry

    2026-07-30

    Enhancing Downstream Bioprocessing with Specialty Chemistry

    Enhancing Downstream Bioprocessing with Specialty Chemistry

    Modern biomanufacturing relies on high-purity n n dimethylbenzylamine catalysts to control pH and accelerate enzymatic transformations during downstream extraction steps. As industrial biotechnology advances from traditional fermentation toward hybrid chemical-biological synthesis, the role of specialized organic media becomes increasingly critical. Bioprocess engineers must balance biological viability with chemical extraction efficiency to isolate high-value metabolites, enzymes, and bio-based polymers at industrial scales.

    images (5).jpg


    Downstream processing frequently accounts for the majority of total manufacturing expenditures in biotech facilities. Choosing optimized solvent systems and organic bases enables selective biomass cell lysis, biopolymer functionalization, and rapid phase separation without damaging delicate protein tertiary structures.

    Solvent Systems for Biomolecule Isolation and Extraction

    Separating hydrophobic target molecules from complex aqueous fermentation broths presents significant engineering challenges. Traditional aqueous two-phase systems often suffer from poor distribution coefficients or low selectivity. Integrating tailored organic solvents with high thermal stability allows engineers to extract target metabolites efficiently while preserving enzyme activity in secondary phases.

    The physical properties of the extraction medium—such as interfacial tension, density differential, and non-corrosive nature—directly govern the separation speed in continuous centrifuges and liquid-liquid extraction columns. Solvents that resist emulsification ensure clean phase boundaries, drastically reducing processing times and energy consumption during solvent recovery.

    Biopolymer Functionalization and Catalytic Engineering

    Bio-based materials such as chitosan, cellulose derivatives, and polyhydroxyalkanoates (PHAs) require chemical modification to enhance their mechanical strength, solubility, or biocompatibility for medical and industrial packaging uses. Tertiary amine catalysts play a vital role in mediating esterification and etherification pathways on bio-polymeric backbones.

    Maintaining precise stoichiometric control during these polymer modifications prevents unwanted chain scission or cross-linking. High-purity catalytic inputs guarantee consistent reaction kinetics, allowing materials scientists to fine-tune the functional properties of bio-based materials for targeted commercial applications.

    Securing High-Specification Raw Materials for Biotech Infrastructure

    Biological systems are uniquely sensitive to chemical contaminants. Trace levels of unreacted toxic compounds, heavy metals, or volatile organic impurities can inhibit microbial cell growth or denature active biocatalysts in bioreactor systems. Biopharmaceutical and industrial biotech firms require a high-quality provider capable of supplying refined chemical agents that conform to rigorous purity specifications.

    Standardized chemical catalysts like triethylenediamine uses underscore the critical overlap between chemical synthesis and biological process engineering. Utilizing certified, stable catalytic media safeguards cellular systems, streamlines purification cascades, and ensures batch-to-batch reproducibility across global production facilities.

    The Future of Integrated Chemical-Biological Systems

    The fusion of biocatalysis and advanced organic synthesis represents a key pathway toward sustainable chemical manufacturing. By leveraging high-selectivity biocatalysts alongside chemically optimized downstream extraction reagents, biomanufacturers can achieve unprecedented yields with minimal carbon impact. Sourcing reliable, high-precision chemical inputs remains fundamental to realizing the full commercial potential of modern biotechnology.

    details
  • Stringent Reagent Purity: The Foundation of Stable Biochemical Synthesis

    2026-07-29

    Stringent Reagent Purity: The Foundation of Stable Biochemical Synthesis

    Stringent Reagent Purity: The Foundation of Stable Biochemical Synthesis

    Sourcing from a China Top Sodium Cyanide Factory is a non-negotiable protocol for laboratories and biochemical synthesis facilities demanding absolute chemical stability. In complex organic synthesis and biological assays, the integrity of the foundational reagents dictates the success of the entire reaction chain. Even microscopic variations in chemical precursors can lead to unwanted byproducts, skewed assay results, or drastically reduced yields.

    e3807baa-45bb-4948-b29b-396475949936.png

    The Threat of Trace Impurities in Synthesis

    When synthesizing complex molecules, scientists must account for every variable. Standard industrial-grade chemicals often harbor fluctuating levels of impurities. For instance, excessive alkalinity from unregulated byproducts can inadvertently alter the pH of a sensitive biological reaction matrix, leading to degradation of the target compound. Therefore, selecting chemical precursors that undergo standardized, rigorous testing against national and international industry standards is paramount for reproducible results.

    Elevating the Supply Chain for Advanced Reagents

    The global biochemical industry relies on a highly specialized supply chain to procure its raw materials. Whether dealing with complex inorganic salts or sourcing from a Top silver Mercury Supplier for specific catalytic applications, the emphasis is always on verified purity. An advanced supplier will utilize automated synthesis lines and provide detailed Certificates of Analysis (COA) for every batch. By guaranteeing a purity level of 98% minimum and tightly controlling physical forms like white crystalline powders for optimal water solubility, these premium manufacturers empower biochemical researchers to push the boundaries of molecular synthesis without second-guessing their foundational materials.

    details
  • The Future of Bio-Fermentation in Livestock Nutrition: A Cellular Perspective

    2026-07-28

    The Future of Bio-Fermentation in Livestock Nutrition: A Cellular Perspective

    The Future of Bio-Fermentation in Livestock Nutrition: A Cellular Perspective

    69c425b237b39.png

    As a nutritional feed additive, advanced bio-fermentation products are revolutionizing modern agriculture. The biological sciences sector has witnessed a massive paradigm shift over the past decade. Instead of relying on traditional bulk feed, the industry is now pivoting toward precision nutrition. This involves the meticulous breakdown of macromolecules into highly bioavailable components, ensuring that young livestock and high-grade aquatic animals can absorb nutrients at the cellular level with minimal metabolic waste.

    The Science of Small Peptides and Amino Acids

    To understand the efficacy of modern nutritional strategies, one must examine the role of small peptides. Unlike intact proteins, which require extensive enzymatic breakdown in the gastrointestinal tract, small peptides (particularly those containing fewer than three amino acids) are absorbed directly through the intestinal enterocytes. This rapid absorption is crucial for young livestock whose digestive systems are not yet fully developed. Research indicates that utilizing specific biological tissues, such as processed sheep intestine or porcine solubles, can yield a product rich in these vital peptides.

    Dried Porcine Solubles (DPS), for instance, can contain more than 70% small peptides. When enriched with trace elements and multi-amino acids, it becomes an unparalleled resource for accelerating growth and maintaining animal health. The biological extraction and fermentation processes dictate the ultimate quality of these elements. This is why agricultural innovators place immense value on the technical capabilities of their supply chain.

    Fermentation Technologies and Ingredient Efficacy

    The core of producing high-efficacy additives lies in the fermentation department. Utilizing high-quality raw materials like corn starch, advanced biological facilities employ multi-stage fermentation, decolorization, and crystallization. This highly controlled biological environment is what transforms basic starches into complex, life-sustaining amino acids and vitamins. By leveraging scientific research achievements from leading universities, the industry can optimize these microbial processes to produce ingredients that bolster the immune systems of vulnerable livestock.

    Supply Chain Excellence and Quality Control

    Integrating these advanced bioproducts into global agricultural systems requires partnering with a sophisticated lysine feed additive manufacturer or similar premium providers. A high-quality provider ensures that the complex biological parameters—such as the concentration of probiotics, the stability of enzymes, and the precise balance of minerals—are maintained from the laboratory to the farm. Cross-border distribution of these biological assets also demands strict adherence to international safety data sheets and phytosanitary regulations. Ultimately, the intersection of advanced bio-science and a premium manufacturing supply chain guarantees the health and optimal status of global livestock populations.

    Conclusion

    The trajectory of animal nutrition is unequivocally leaning toward biologically refined, highly bioavailable additives. By focusing on cellular absorption, leveraging local premium raw materials, and maintaining uncompromising standards in fermentation technology, the modern agricultural sector can achieve unprecedented levels of efficiency and animal welfare.


    details

If you are interested in our products, you can choose to leave your information here, and we will be in touch with you shortly.