Kaolin Clay is a cornerstone material in the chemical industry, valued for its inertness, whiteness, and fine particle size. From ceramics and paints to pharmaceuticals and rubber, this layered silicate mineral provides essential functional properties that manufacturers depend on for consistent product quality.
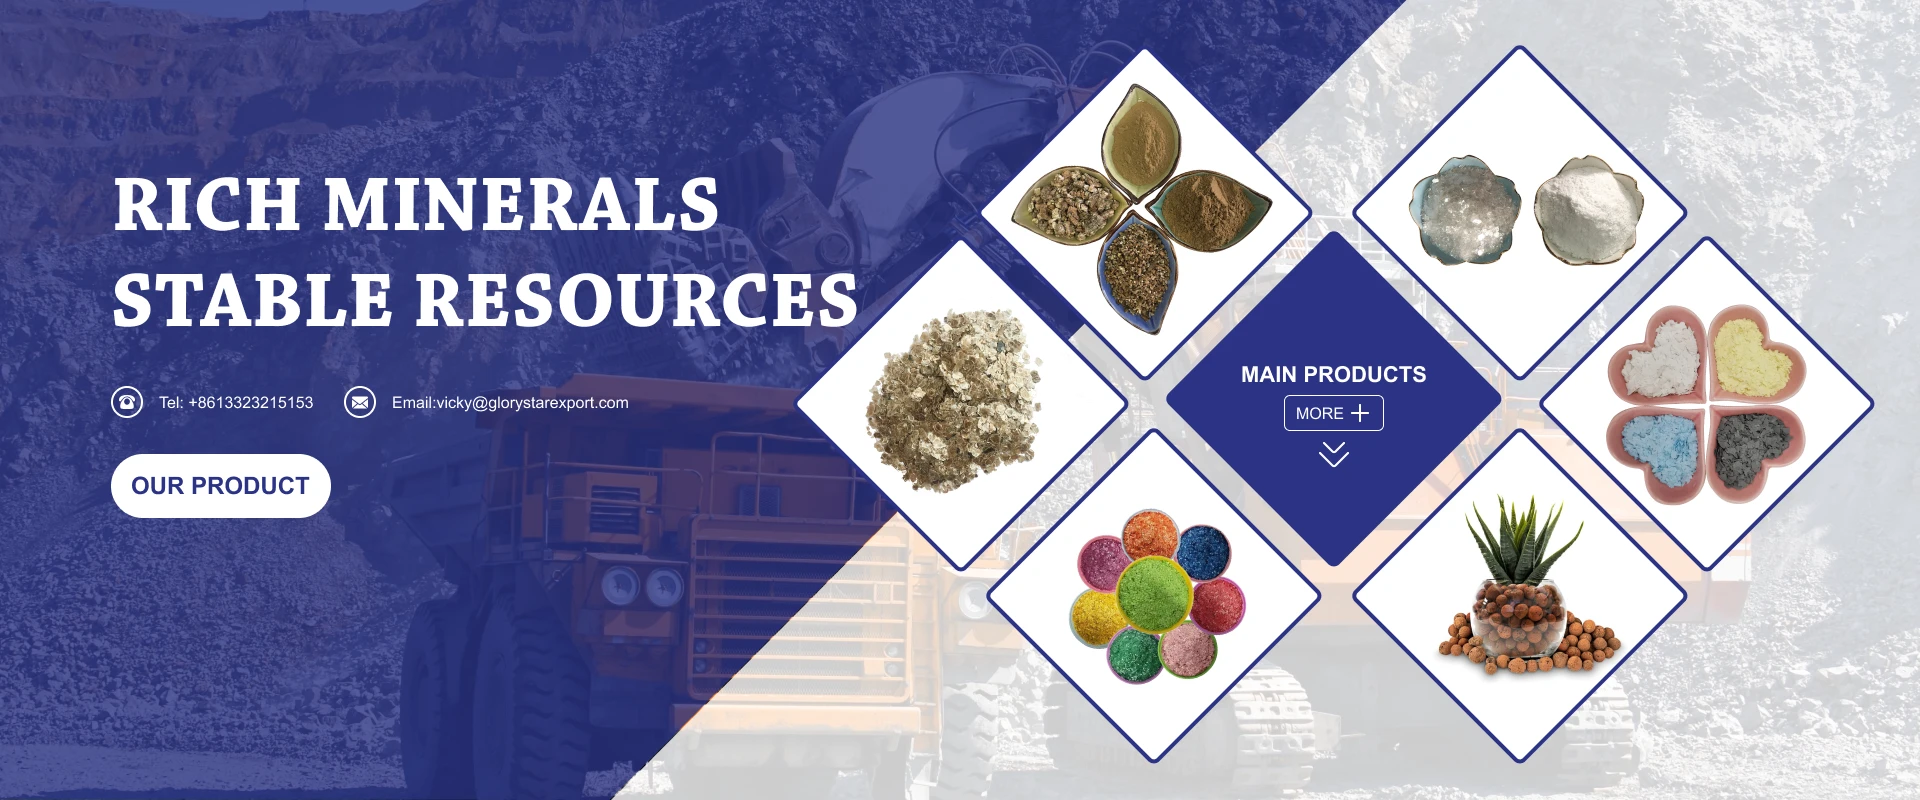
Beyond kaolin, the broader family of non-metallic minerals — including bentonite, talc, diatomite, calcium carbonate, and barite — serves as the hidden backbone of countless chemical formulations. These raw materials influence everything from viscosity and opacity to thermal stability and abrasion resistance. As global chemical manufacturers push for higher performance and tighter regulatory compliance, the quality and consistency of these mineral inputs have never been more critical.
Why Raw Material Quality Shapes Finished Product Performance
In chemical manufacturing, the journey from raw material to finished product passes through multiple stages where variability can compound. A slight shift in mineral particle size distribution or trace element composition can alter reaction kinetics, change color profiles, or weaken structural integrity. This is why leading producers implement rigorous, multi-stage quality control systems that test incoming raw materials, in-process slurries, and final stored product before shipment.
The most reliable mineral suppliers follow a four-point inspection protocol: first, testing raw materials upon arrival at the plant; second, conducting quality checks during active production; third, verifying specifications before warehouse storage; and fourth, performing a final spot check prior to loading. This layered approach, often aligned with ISO 9001:2015 management systems, minimizes the risk of off-spec material reaching the customer.
Key Industrial Minerals and Their Chemical Applications
Different minerals bring distinct value to chemical processes. Bentonite, with its high swelling capacity and ion-exchange properties, is widely used as a binder, thickener, and suspending agent in drilling fluids, foundry sands, and cosmetic formulations. Talc powder contributes lubricity, thermal stability, and reinforcement in plastics, paper, and coatings. Diatomite, a naturally porous silica, serves as a filtration aid, absorbent, and mild abrasive. Calcium carbonate, one of the most abundant minerals on earth, functions as a filler, extender, and pH buffer in paints, adhesives, sealants, and pharmaceuticals.
Graphite Powder is another versatile material with growing importance in the chemical sector. Its high thermal conductivity, chemical inertness, and natural lubricity make it indispensable in high-temperature gaskets, conductive coatings, battery electrodes, and specialty lubricants. As the energy transition accelerates demand for advanced battery materials, the role of high-purity graphite continues to expand.
Supply Chain Reliability in a Global Market
Chemical manufacturers today face mounting pressure to secure stable, long-term supplies of high-quality mineral raw materials. Geopolitical disruptions, logistics bottlenecks, and variable ore grades from one region to another all introduce risk. Experienced buyers look for suppliers with deep reserves, established production history, and a track record of consistent export to demanding markets such as Japan, South Korea, the United States, Germany, and Australia.
One noteworthy example is the Lingshou County region in China, a historic source of non-metallic minerals including mica, kaolin, and graphite. Factories with decades of operational experience, backed by dedicated R&D teams and national high-tech certifications, offer the kind of technical stability that global chemical buyers require. The presence of multiple national patents and active membership in local mineral associations further signals a commitment to continuous improvement and industry standards.
Selecting the Right Mineral Partner for Long-Term Success
When evaluating mineral suppliers, chemical manufacturers should prioritize three factors: demonstrated quality systems, production capacity, and technical expertise. ISO 9001 certification provides a baseline for process control, but the most reliable partners go further by investing in in-house testing laboratories and developing customized product grades for specific applications. A supplier with annual output exceeding 100,000 metric tons and a 35-year-plus operating history brings both scale and institutional knowledge that smaller operations cannot match.
As the chemical industry continues to evolve — toward greener formulations, higher purity standards, and more complex performance requirements — the importance of high-quality mineral raw materials will only grow. By choosing partners who invest in technology, quality control, and long-term relationships, manufacturers can build supply chains that are both resilient and capable of supporting the next generation of chemical products.